Request a quote


At LabSPX, we are committed to bringing innovative and efficient solutions to laboratories. Our Smart Lab Solutions are designed to streamline processes, enhance accuracy, and boost productivity.
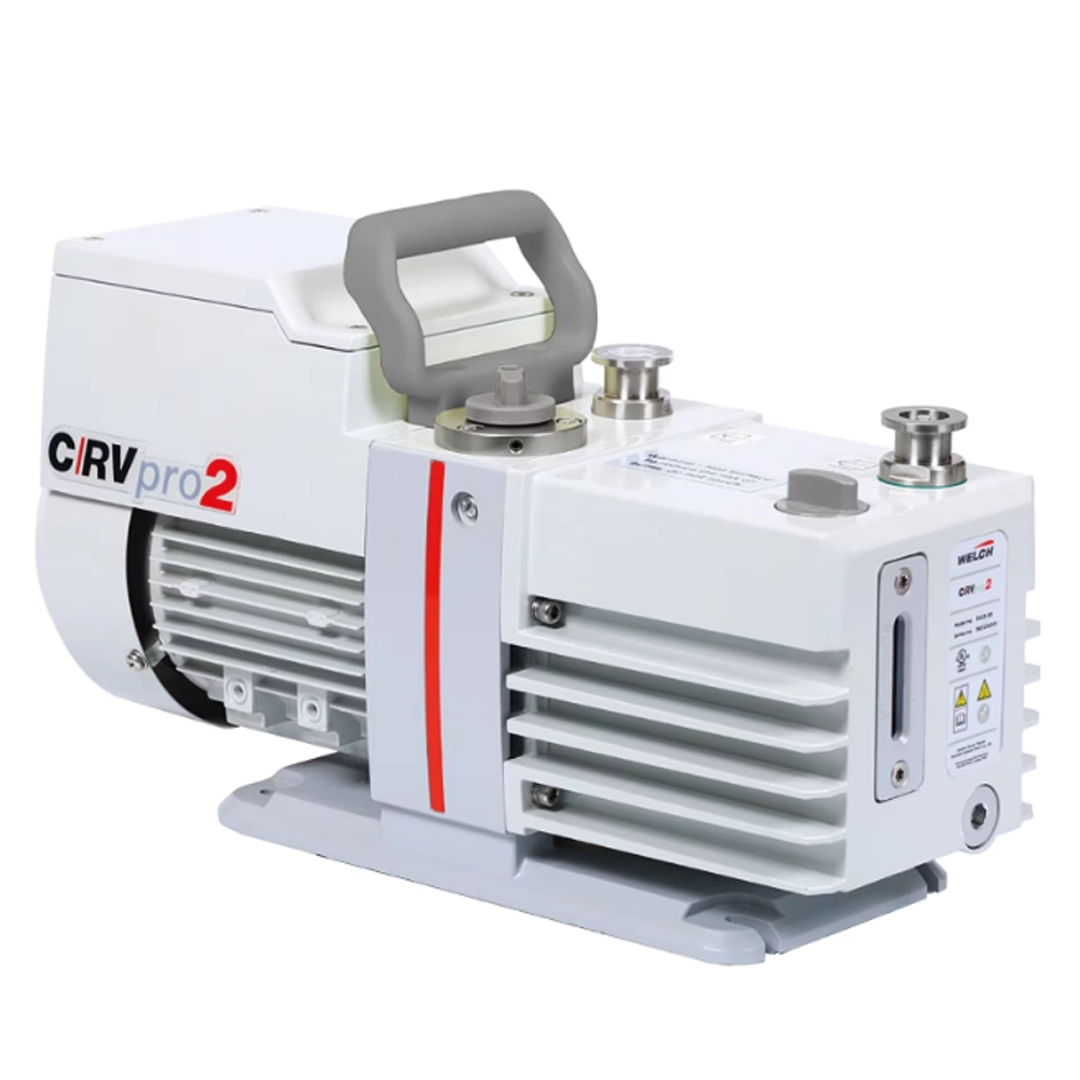
These Piston Vacuum Pumps are fully equipped, durable, and oil-free. They are developed for standard-duty applications where corrosion resistance is not essential, such as filtration, gas sampling, vacuum drying, and automation technology. They use a dedicated piston mechanism to generate vacuum.
These pumps are suitable for a wide range of applications involving physical and aqueous vapor applications. They are ideal for many standard-duty applications in both laboratory and industrial settings, including:
Laboratories: used for sample preparation, controlled environments, and filtration in scientific workflows such as DNA/RNA extraction
Analytical instruments: support accurate measurements in instruments like gas chromatographs and spectrometers
Industrial manufacturing: applied in vacuum drying, casting, and packaging processes to improve product quality
Pharmaceuticals: essential for processes such as freeze-drying and solvent removal, helping maintain product purity and stability
Food processing: contribute to high-quality packaging and processing, preserving flavor and extending shelf life
Automotive testing: used for brake system testing, emissions control, and leak detection
Research facilities: support a wide range of experiments, including mass spectrometry and electron microscopy
HVAC systems: used to evacuate and maintain vacuum in refrigeration and air conditioning systems
Environmental monitoring: enable accurate air and gas sampling for pollution monitoring and assessment
Material handling: remove air and gases during molding and curing processes
Enhanced performance: exceptional vacuum and flow in a compact design, ensuring reliable performance across a variety of applications
Dependable operation: made with high-quality materials and innovative design features, these pumps minimize maintenance and provide long-lasting, reliable operation
Controlled vacuum: equipped with regulators and gauges, these pumps allow easy adjustment and monitoring of vacuum levels for precise, application-specific control
Protection mechanism: an inlet water trap prevents accidental water intake, maintaining pump performance even under challenging conditions
Motor safety: all models feature single-phase motors with built-in thermal overload protection, adding an extra layer of safety to your vacuum operations
Oil-free piston pumps offer several advantages for your operations:
Environmentally friendly: by eliminating the need for lubricating oil, these pumps reduce the risk of oil contamination, creating a cleaner workplace
Cost savings: no oil means lower expenses for purchase, handling, and disposal, reducing overall operating costs
Easy maintenance: these pumps require less maintenance than oil-based alternatives, resulting in less downtime and higher productivity
Improved product purity: oil-free operation prevents oil contamination, making these pumps ideal for applications that demand the highest level of purity
Lower operating temperatures: running without oil keeps pumps cooler, extending component life and increasing overall reliability
Single-head pumps:
Dual-head pumps:
Explore similar solutions and complementary products.